
Two Colour Industrial Bag Printing Solutions for Modern Packaging Manufacturers
By Rentech Machine Private Limited
Transforming Ready-Made Bags into Professionally Branded Packaging
In the modern packaging industry, the appearance of a bag plays an important role in product marketing, brand recognition and customer perception. Packaging manufacturers are no longer focused only on producing bags for carrying and storing products. They are also expected to deliver customised packaging that represents their customers' brands and business identities.
From agricultural packaging and industrial sacks to retail shopping bags and promotional fabric bags, printed packaging is becoming an important requirement across multiple industries.
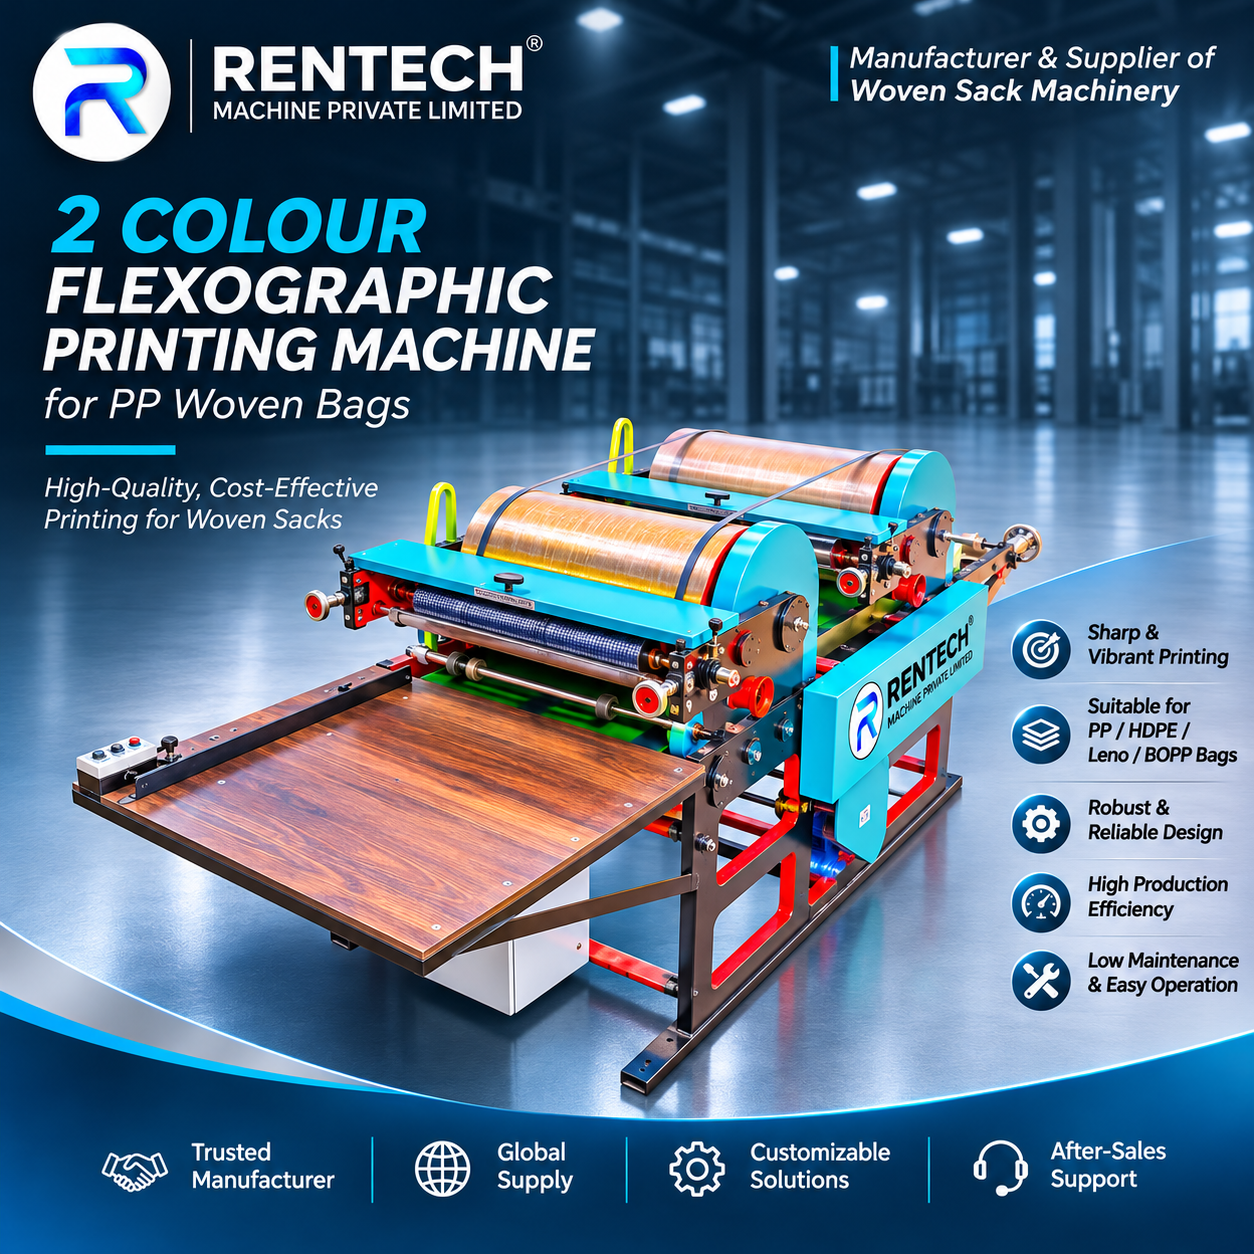
To address these requirements, Rentech Machine Private Limited offers a Two Colour Bag-to-Bag Printing Machine designed for printing on suitable ready-made bags made from different materials, including PP woven, HDPE, paper, kraft paper, jute, non-woven and canvas cotton.
The machine provides a practical printing solution for manufacturers who want to offer customised bag printing without depending entirely on pre-printed roll materials. It enables businesses to explore different customer requirements, branding applications and packaging markets through a single printing solution, subject to material and printing-process compatibility.
A Versatile Printing Solution for Different Packaging Materials
Every packaging material has different characteristics. PP woven fabric, HDPE, paper, jute and cotton fabrics differ in surface texture, ink absorption and printing behaviour.
For this reason, choosing the right printing arrangement is important for achieving consistent results.
The Two Colour Bag-to-Bag Printing Machine is intended to support different bag printing applications, helping manufacturers serve customers from agricultural, industrial, retail, textile and commercial packaging sectors.
The two-colour arrangement allows businesses to reproduce designs using two colours, making it suitable for brand names, company logos, product descriptions, promotional graphics and other packaging information.
Rather than limiting production to a single type of packaging, manufacturers can explore multiple market segments according to their printing requirements.
Printing Applications Across Different Bag Industries
PP Woven Bag Printing – Branding for Agricultural and Industrial Packaging
PP woven bags are widely used for packaging rice, wheat, sugar, fertilisers, animal feed, seeds, chemicals and other industrial products.
In these industries, packaging is an important source of product identification. Manufacturers and distributors require their company names, product details, logos and handling instructions to be clearly visible.
A two-colour bag printing solution helps PP woven bag manufacturers offer customised packaging to different customers. It can also support businesses that handle multiple product categories and require different printed designs.
HDPE Bag Printing – Practical Printing for Commercial Packaging
HDPE bags are used in various packaging and industrial applications where strength, durability and functional packaging are important.
Printing on suitable HDPE bags allows businesses to display product information, company branding, identification details and promotional designs.
The printing process should be selected according to the surface characteristics and treatment of the HDPE material to achieve suitable ink adhesion and print quality.
Paper Bag Printing – Professional Packaging for Retail Businesses
Paper bags are commonly used by supermarkets, grocery stores, retail outlets, restaurants, shopping brands and commercial businesses.
Customised printing helps businesses convert ordinary paper bags into branded packaging products.
A two-colour printing arrangement can reproduce attractive logos, business names, promotional messages and product-related information. This creates additional opportunities for paper bag manufacturers supplying customised packaging to different customers.
Kraft Paper Bag Printing – Combining Packaging and Brand Identity
Kraft paper bags have become an important packaging choice for retail stores, food businesses, shopping brands and various commercial applications.
Their natural paper appearance provides an attractive background for simple and bold printing designs.
Two-colour printing can be used for business logos, product descriptions, brand names and promotional messages. This helps kraft paper bag manufacturers offer customised packaging solutions for businesses looking to improve their product presentation.
Jute Bag Printing – Custom Branding on Natural Fibre Packaging
Jute bags are widely used in shopping, agriculture, promotional packaging, gift packaging and reusable packaging applications.
Businesses often prefer printed jute bags for corporate branding, retail promotions and customised packaging.
Printing on jute requires attention to its woven and textured surface. Suitable printing arrangements, ink selection and sample testing are important for achieving the required appearance.
Non-Woven Bag Printing – Promotional and Reusable Shopping Bags
Non-woven bags are popular in supermarkets, retail stores, exhibitions, promotional campaigns and corporate events.
Their reusable nature makes them an attractive option for businesses that want their branding to remain visible beyond the initial purchase.
A two-colour printing process can help non-woven bag manufacturers produce customised shopping bags carrying company logos, brand names and promotional artwork.
This application offers opportunities for manufacturers serving retail, advertising and promotional merchandise businesses.
Canvas Cotton Bag Printing – Customised Packaging for Premium Brands
Canvas and cotton bags are widely used in fashion retail, lifestyle stores, corporate gifting, exhibitions and promotional merchandise.
These bags provide businesses with an opportunity to combine reusable packaging with customised brand communication.
Printing can be used for company logos, creative artwork, promotional messages and retail branding. Since cotton and canvas surfaces have different absorption characteristics, suitable ink selection and printing trials are recommended before commercial production.
Why Are Manufacturers Moving Towards Ready-Made Bag Printing?
Traditional packaging production often involves printing on material rolls before converting them into finished bags. Although this process is suitable for many production requirements, it may not always be convenient for manufacturers handling multiple customer designs and smaller customised orders.
Bag-to-bag printing provides another approach by allowing printing on already manufactured bags.
This can offer several operational advantages.
Greater order flexibility: Manufacturers can handle different customer artwork and branding requirements without necessarily maintaining separate pre-printed stock for every design.
Improved customer service: Packaging businesses can offer customised printing services to customers who require their company logos, product details and promotional information.
Expansion into additional markets: Existing bag manufacturers can explore printing applications across PP woven, paper, jute, non-woven and fabric bag segments.
Better packaging presentation: Professionally printed bags can improve the visual identity of products and help businesses present their brands more effectively.
Additional business opportunities: Manufacturers can consider adding bag printing as a value-added service alongside their existing bag manufacturing and conversion activities.
The Importance of Selecting the Right Printing Process
Printing on different materials requires careful consideration. A printing solution suitable for PP woven bags may not automatically deliver the same results on cotton, jute or kraft paper.
Several factors influence the final printing quality:
- Surface condition and treatment of the bag.
- Material thickness and texture.
- Ink compatibility and adhesion.
- Artwork design and colour combination.
- Printing alignment and positioning.
- Drying requirements.
- Required appearance and durability of the printed design.
For this reason, manufacturers should evaluate actual bag samples before finalising the printing arrangement for different materials.
Rentech Machine Private Limited recommends discussing material specifications and printing requirements before selecting the appropriate machine configuration.
How Can Bag Manufacturers Expand Their Business with Two Colour Printing?
The packaging market includes customers with different requirements. A fertiliser manufacturer may need branded PP woven sacks, while a retail business may require printed kraft paper bags. A promotional company may be looking for customised non-woven or canvas cotton bags.
These different requirements create opportunities for packaging manufacturers to expand beyond a single product category.
By introducing suitable bag-to-bag printing facilities, manufacturers can explore customised orders and provide additional services to their existing customers.
This approach can be particularly useful for businesses that already manufacture plain bags and want to enter the customised packaging segment.
Why Choose Rentech Machine Private Limited?
Rentech Machine Private Limited is engaged in manufacturing machinery solutions for the woven sack, bag conversion and packaging industry.
Our product range includes bag cutting and stitching machinery, flexographic printing machinery and woven bag conversion solutions.
We understand that packaging manufacturers require equipment that supports their production requirements and business expansion plans.
Our Two Colour Bag-to-Bag Printing Machine is intended for businesses looking for a versatile printing solution for suitable ready-made bags across different material categories.
We focus on providing practical machinery solutions for manufacturers who want to improve their production capabilities, introduce customised printing services and serve a wider customer base.
Whether you are an established PP woven sack manufacturer, a paper bag producer or a business planning to enter the non-woven and fabric bag printing segment, Rentech Machine Private Limited can help you explore suitable printing machinery solutions.
Rentech Machine Private Limited – Engineering Machinery Solutions for the Evolving Packaging Industry.
Frequently Asked Questions (FAQs)
What is a Two Colour Bag-to-Bag Printing Machine?
It is an industrial printing machine designed to print directly on ready-made bags using two printing colours. It is used for printing company logos, brand names, product information, promotional designs and other customised artwork.
Which types of bags can be printed using this machine?
The machine is intended for suitable PP woven bags, HDPE bags, paper bags, kraft paper bags, jute bags, non-woven bags and canvas cotton bags. Actual suitability depends on material characteristics, ink compatibility and machine configuration.
Can the machine print directly on ready-made bags?
Yes. Bag-to-bag printing is designed for printing on individual converted bags rather than requiring printing on continuous material rolls before bag manufacturing.
Is this machine suitable for PP woven sack manufacturers?
Yes. It can be considered by PP woven sack manufacturers who require customised printing for fertiliser, rice, sugar, grain, animal feed and other industrial packaging bags.
Can I use this machine for paper and kraft paper bags?
Suitable paper and kraft paper bags can be considered for printing. The printing arrangement and ink should be selected according to the paper surface and required print finish.
Is jute bag printing possible?
Yes, suitable jute bags can be evaluated for printing. Due to the textured surface of jute fabric, sample testing is recommended to determine the appropriate printing process and ink.
Can non-woven shopping bags be printed?
Yes. Suitable non-woven bags can be used for printing company branding, retail logos, promotional messages and customised designs.
Can canvas and cotton bags be used for printing?
Canvas and cotton bags can be considered, depending on their construction, surface properties and printing requirements. A printing trial is advisable before commercial production.
What are the benefits of two-colour printing?
Two-colour printing allows manufacturers to create designs using two separate colours. It is useful for logos, product names, branding, promotional artwork and packaging information.
Can different customer designs be printed on different bags?
Yes. The bag-to-bag printing approach is suitable for customised customer orders. Manufacturers can prepare different designs according to customer artwork and production requirements.
Which industries can benefit from this printing machine?
Agriculture, fertiliser, food grain, sugar, animal feed, retail, shopping, paper packaging, jute packaging, non-woven bag manufacturing and promotional merchandise industries can explore this printing solution.
How can I select the right bag printing machine?
Consider the bag material, dimensions, surface properties, printing area, required colours, production expectations and ink compatibility. Providing actual bag samples and printing artwork helps the manufacturer recommend an appropriate configuration.
How can I get a quotation from Rentech Machine Private Limited?
Contact Rentech Machine Private Limited with your bag material, bag dimensions, printing requirements and expected production capacity. Our team can discuss the suitable machine configuration and provide quotation details.